Chrome does three things at once: it resists corrosion, it resists wear, and it releases the web. That combination is why chrome rollers dominate coating, laminating and drying sections.
The plating is only as good as the base. We grind before plating and inspect after, because a chrome layer over a poor surface
Values marked “to be confirmed” are set against the factory’s tested capability before quotation. Send your dimensions and we will confirm against them. Yes, if the base is sound. The old layer is stripped, the surface re-ground, then re-plated and finished. If the base is corroded or pitted, a new core is usually cheaper than repair. Mirror for release and coating uniformity where surface texture transfers to the web. Matte where you need slight grip or where scratches would be visible on a mirror finish. 25–50 micron covers most applications. Thicker is not automatically better: it costs more, takes longer and can build stress. Tell us the wear mechanism and we will specify. Email your drawing, the machine model, or photos of the roller you need replaced. You will get a material proposal, a price and a lead time.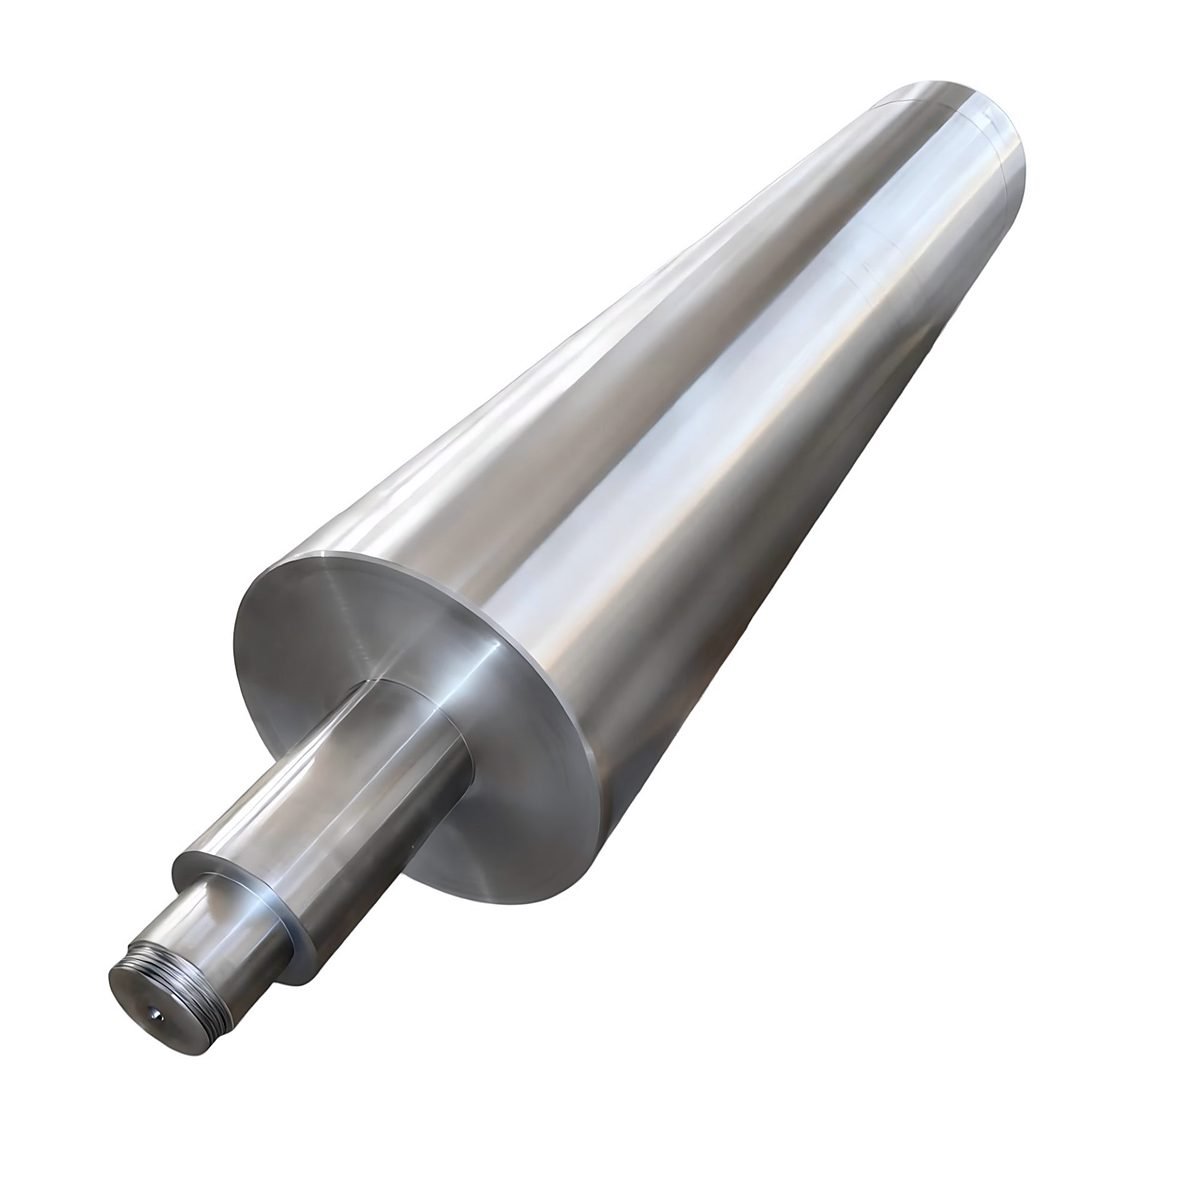
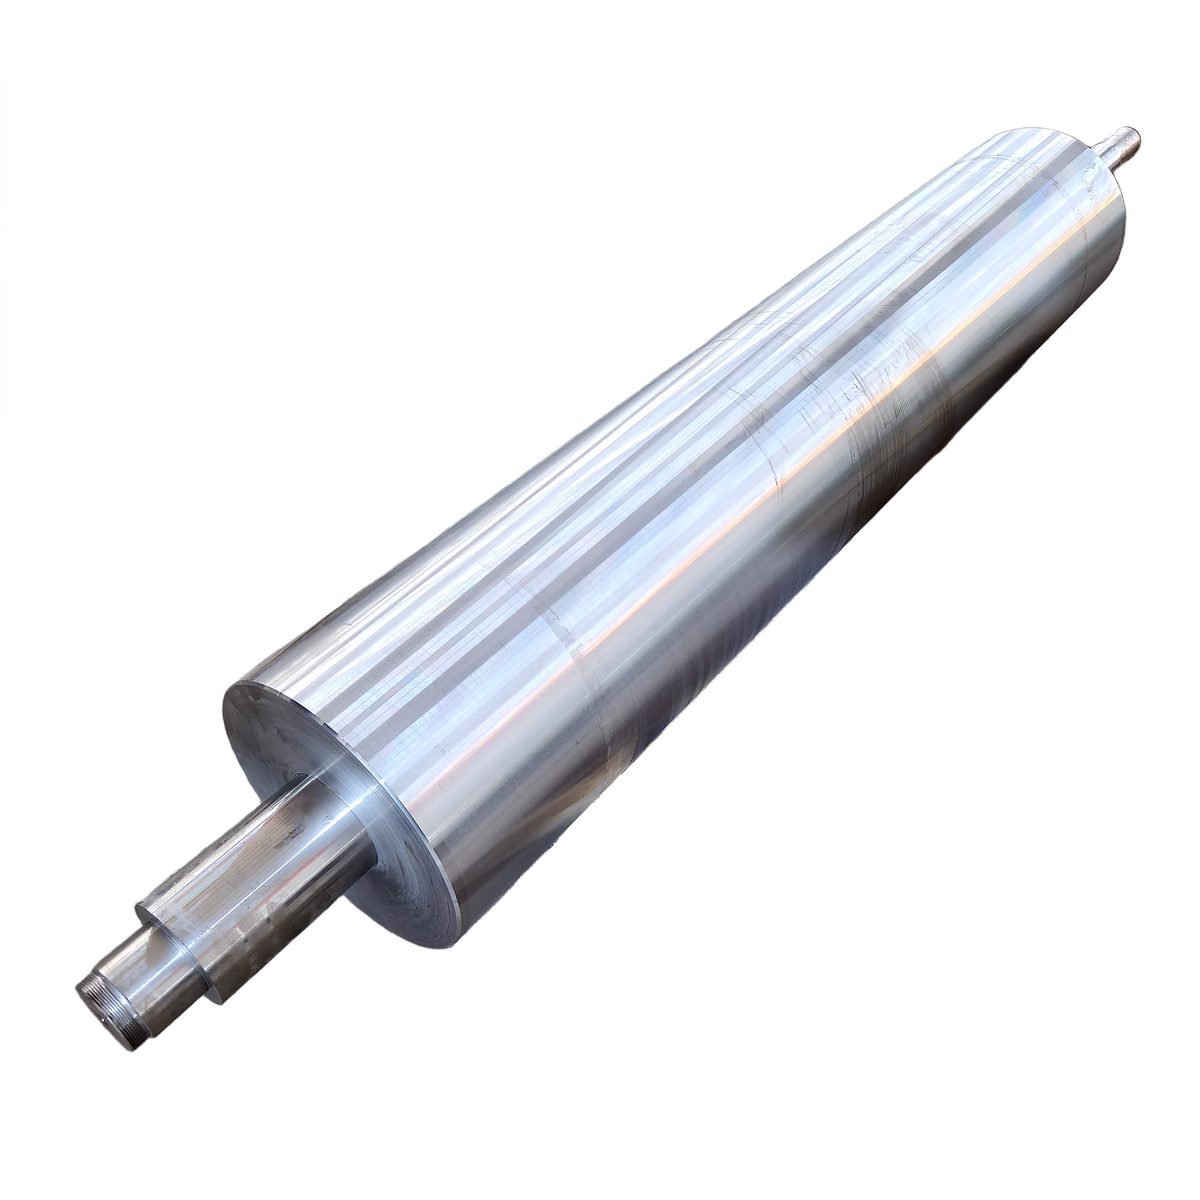
What We Can Build
Parameter Range / option Base material Carbon steel, stainless steel Plating thickness 20–100 micron, typical 25–50 micron Surface finish Mirror (Ra 0.05–0.2) or matte Hardness of plating to be confirmed (typically 800–1000 HV) Outside diameter to be confirmed Face length to be confirmed Corrosion resistance Salt spray hours to be confirmed Where These Rollers Are Used
Chrome Plated Roller Questions
Can you re-plate an existing chrome roller?
Mirror or matte — which do I need?
How thick should the chrome be?
Send the Drawing or the Worn Roller